Piab Premium piFLOWp Vacuum Conveyor
Piab Premium piFLOW p
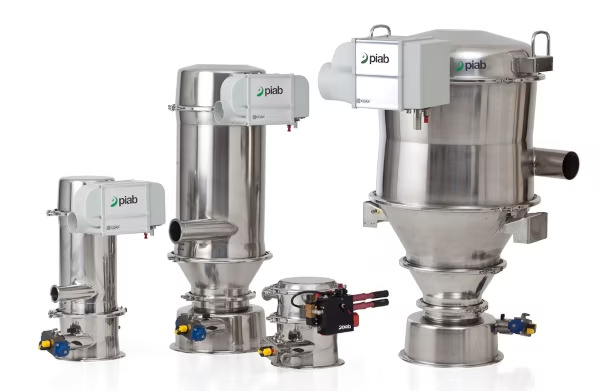
The Piab Premium piFLOW®p is the ideal vacuum conveyor when premium technology is required, particularly in the food and pharmaceutical industries. It is also perfect for applications with high throughput demands while maintaining a compact footprint. These Piab vacuum conveyors come with an ejector-driven vacuum pump or a mechanical pump, ensuring versatility for various industrial applications.
Why Choose R-CAP Process Equipment?
At R-CAP Process Equipment, we provide top-tier industrial process solutions designed to optimize your liquid and dry processing operations. From Admix high shear mixers to Piab vacuum conveyors and integrated process systems, our range of products ensures maximum efficiency, reliability, and precision.
Applications of Piab Vacuum Conveyors
The Piab piFLOW®p is engineered to optimize industrial vacuum conveying across multiple sectors.
- Food & Beverage Processing – Safe and sanitary transfer of ingredients
- Pharmaceutical & Chemical Industries – Precision handling of powders and sensitive products
- Brewing & Distilling – Efficient movement of grains and malt using a brewery pump cart
- Manufacturing & Packaging – Streamlining bulk material movement for big bag unloading and form-fill-seal operations
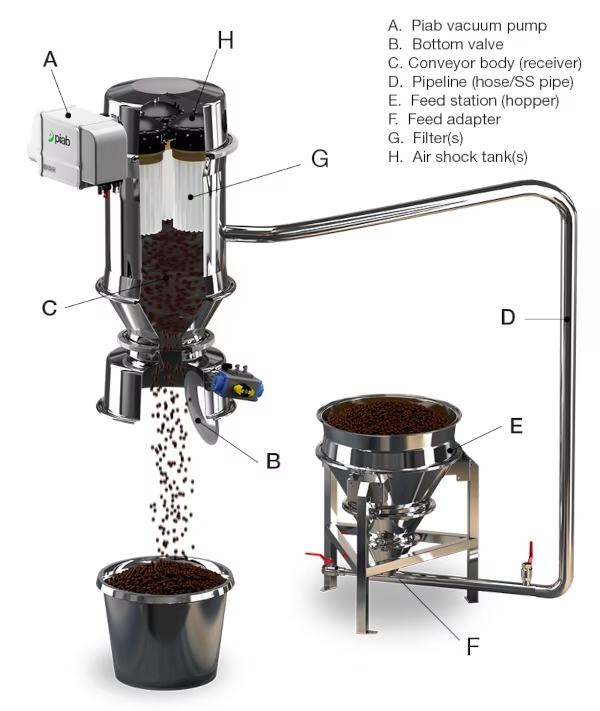
Features & Benefits of the Piab piFLOW p Conveyor
- High-efficiency vacuum technology for superior powder and granules transfer
- Stainless steel construction (ASTM 316L) meeting FDA hygienic standards
- ATEX Dust and Gas certified for explosive atmosphere applications
- Compatible with form-fill-seal machines, big bag loading/unloading, drum/bag filling & emptying
- Seamless integration with mill, sieve, mixer, and blender filling operations
- Gentle handling for tablet and fragile product transfer
- Designed for hygienic applications and space-constrained environments
Upgrade Option: Compatible with Next-Gen Piab piEVO Ejector Pumps
This conveyor system fully integrates with piab’s next-generation piEVO vacuum ejector pump platform, offering a direct upgrade path to improve system uptime and line response.
Key Advantages
Seamless Retrofits: Twist-lock bayonet flange and unified multi-line quick connectors enable rapid, one-handed installation and simplified pneumatic disconnection.
Stable Throughput & Low Noise: Advanced vacuum control delivers faster response times and reliable transfer rates at operating sound levels below 78 dB.
Reduced Maintenance Downtime: Open-cell PUR silencer and ejector modules are easily accessible using standard tools, accelerating service cycles.
100% Serialized Traceability: Every unit features registered serial-number tracking linked to MyProduct/MyPiab for instant configuration lookup, faster field troubleshooting, and exact spare parts ordering.
Built-In System Protection: Integrated blow-off functions and non-return safety valves come standard with full CE, REACH, and RoHS compliance.

Additional Equipment & Integration
Pair the Piab Premium piFLOW®p with other high-performance solutions from R-CAP Process Equipment:
-
- Piab vacuum conveyor accessories: Piab filters, Piab parts for enhanced performance
- Mixing Equipment: Compatible with Admix high shear mixers, DynaShear, Rotostat, and Boston Shear Mill
- Temperature Control Solutions: Works seamlessly with Sterling Chiller, Sterling TCU, and TC 130 for thermal regulation
- Process Optimization: Ideal for use alongside Pentair Sudmo butterfly valves, Pentair Sudmo mixproof valves, and plate and frame heat exchangers